Missing Component Inspection FAQs
Straight answers to common questions about missing component inspection, including suitable applications, limitations and what to send us.
Useful answers about missing component inspection depend on your application, operating range and the results you need.
Your final missing component inspection scope must also account for recipe, variant, reject and line-control interfaces, false-accept, false-reject and challenge criteria, current regulations and the conditions at your site.
Get practical answers for your application — Missing Component Inspection
Plan missing-component inspection around a defined component list, visible verification features, representative complete and incomplete assemblies, stable presentation, reject handling and agreed challenge evidence. The answers below explain suitable applications for Missing Component Inspection, what information helps and what still needs an application-specific check.
Discuss your application
Practical answers about missing component inspection
How can a vision system check that all required components are present?
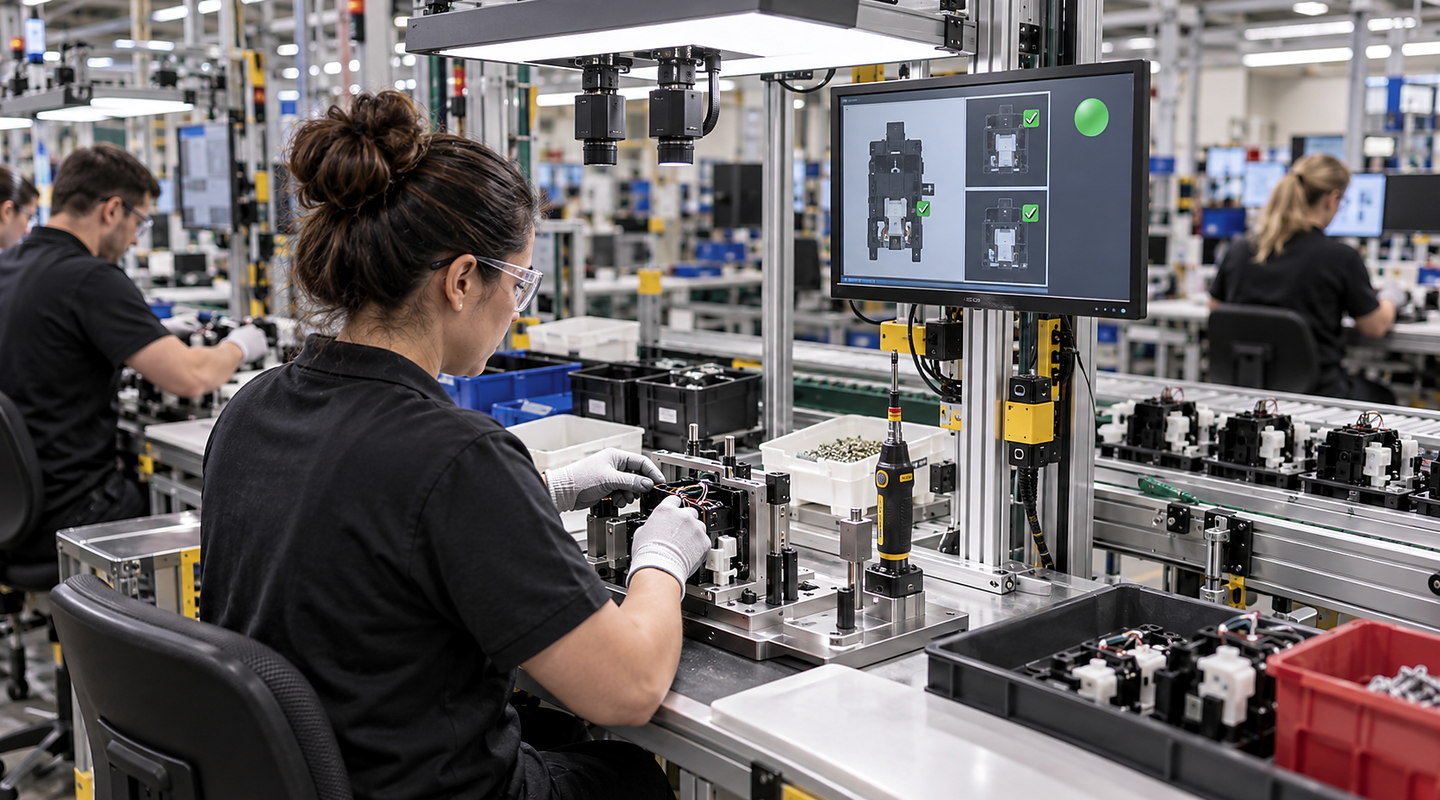
For missing component inspection, define required components and visible verification features and collect complete, missing, misplaced and marginal sample range before choosing cameras. An optical trial should prove contrast, presentation and timing, followed by agreed checks for false-accept, false-reject and challenge criteria.
How should a project for missing component inspection begin?
Define the real duty and collect representative samples or observations. Record required components and visible verification features, complete, missing, misplaced and marginal sample range, and assembly presentation, datum stability and production speed before choosing an approach.
Can you quote missing component inspection from a short description?
An early budget range may be possible, but a reliable scope for in-line verification that required assembly components are present needs the product or part range, line connections, site conditions and your requirements for false-accept, false-reject and challenge criteria.
What information should we send about missing component inspection?
Share authorised drawings or photographs, representative examples from in-line verification that required assembly components are present, current process data, your production pattern, available services, space and known safety or quality requirements.
How will performance be checked?
Use an agreed trial covering normal, difficult and fault conditions for in-line verification that required assembly components are present. Judge the complete system using the agreed requirements for false-accept, false-reject and challenge criteria, not a catalogue maximum.
What are the main limitations?
A camera can only verify a component when a reliable feature is visible. Occlusion, datum shift and normal appearance variation can hide or mimic a missing component. A visible presence result does not prove hidden bond, electrical or mechanical function.
What alternatives should be considered for in-line verification that required assembly components are present?
Compare purpose-built sensors for simple presence or position checks with offline metrology or destructive tests where the property is not visible inline. For Missing Component Inspection, the practical option may be simpler than the most automated one.
Can the proposed solution guarantee regulatory compliance?
No solution can guarantee compliance on its own. Applicable law, current standards, risk assessment, validation and conformity responsibilities must be addressed for your complete application.
Who will handle my enquiry?
Oxford Vision Systems will receive enquiries from missingcomponentinspection.co.uk. Call 01865 416657 or email sales@oxfordvisionsystems.co.uk to speak with the team directly.
Questions to resolve before specification
Visible decision features, occlusion, datum variation and complete/missing/misplaced sample evidence—not generic machine vision. The final decision should use representative evidence from the intended production duty.
Can a camera verify a component that is hidden after assembly?
Only if an independently validated visible proxy exists; otherwise inspect earlier or use another method.
Can the same inspection handle several assembly variants?
It may, but each recipe, feature set, changeover and wrong-variant condition needs representative evidence.
Can one camera check every side of an assembly?
Not necessarily; coverage depends on geometry, occlusion, presentation and required features.
What samples are needed for a feasibility trial?
A useful assessment set includes representative complete, missing, misplaced, marginal and normal-variation examples across variants.